From Manual to Automatic: Why the Color Sorter Machine Is a Must-Have in Modern Food Processing
Entering a modern food processing plant, you will observe that the food processing industry is undergoing a transition from a labor-intensive model to an automated one.
As the global supply chain places increasingly stringent requirements on food safety, the traditional labor-intensive sorting methods have reached their limit.
Manual sorting is not only limited by human visual fatigue but also cannot maintain consistent standards under high-intensity conditions. A tiny mold spot or a slightly darker stone, if missed during inspection and allowed to enter the finished product, could mean the return of the entire batch of goods, or even a devastating blow to the brand reputation.
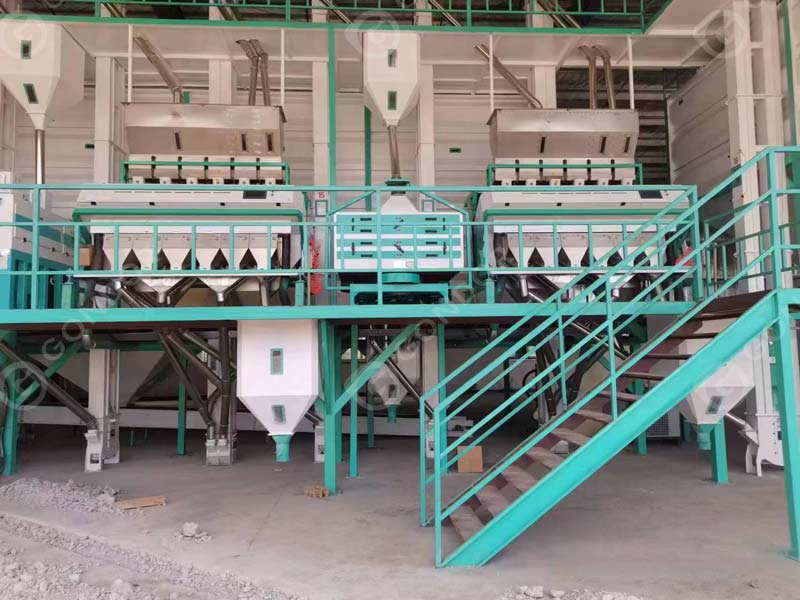
We believe that shifting from manual to automatic production is not merely about purchasing a machine; it is a fundamental transformation concerning production efficiency and quality control. Color sorter machines are precisely the “gatekeepers” in this transformation.
The Core Technology of the Color Sorter Machine
Why can the grain color sorter for sale perform better than humans? This is due to its “sharp eyes”.
Micro-Defect Detection in Milliseconds
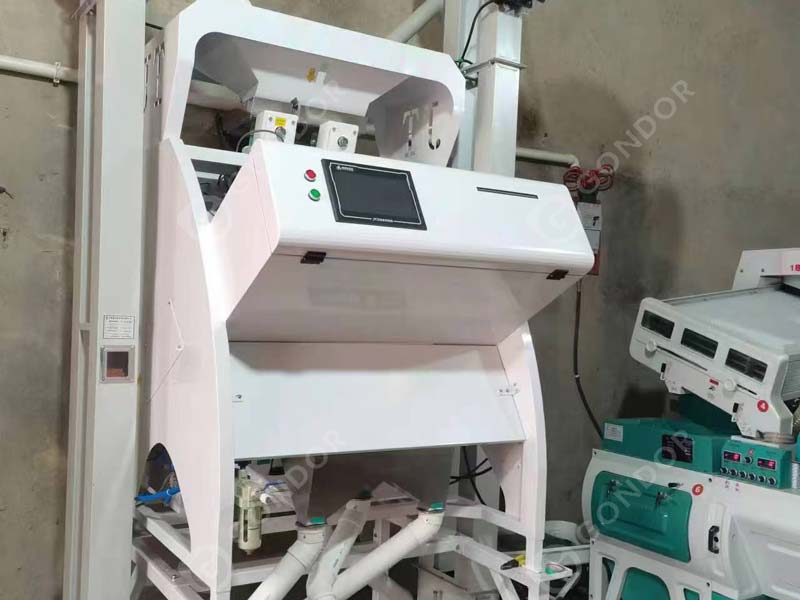
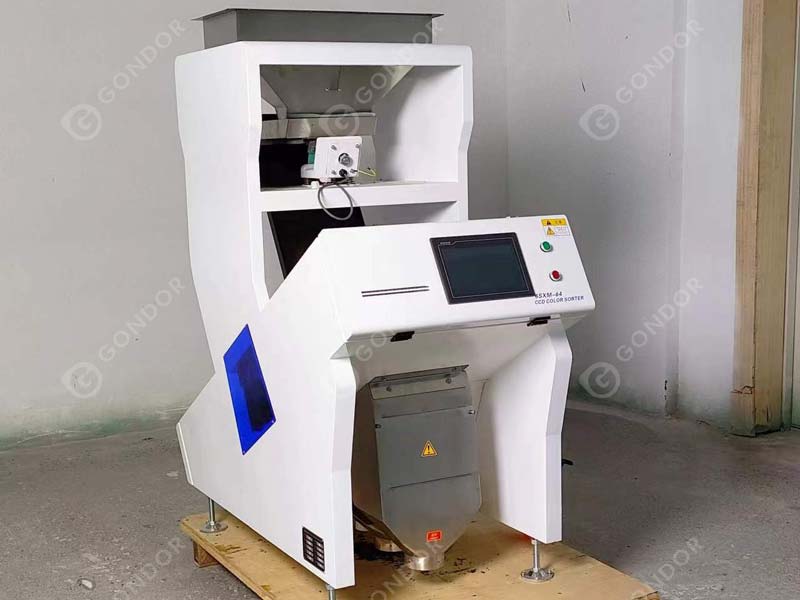
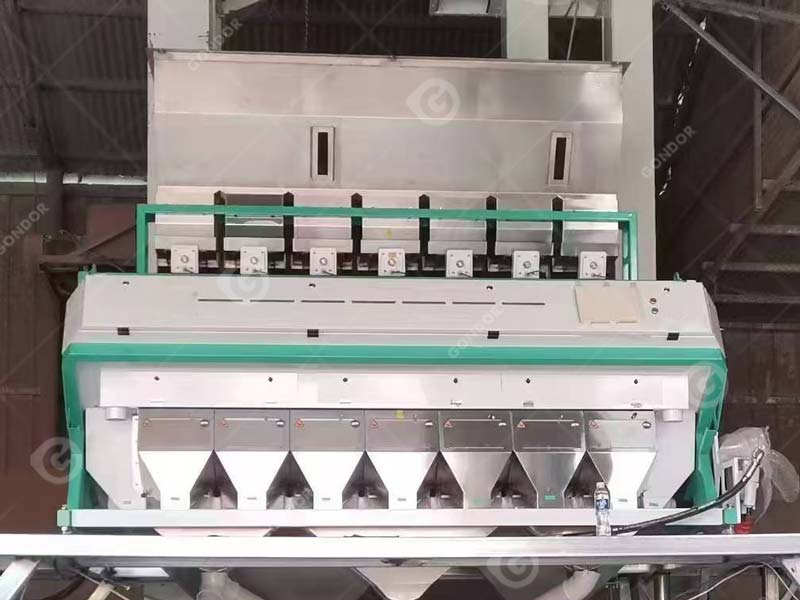
The Gondor best color sorter machine is equipped with an industrial-grade high-resolution CCD camera. This is not just about taking pictures; it can scan the materials at a rate of tens of thousands of times per second.
For those slight color differences that are hard to detect with the naked eye, or tiny spots caused by mold, the system can identify them and issue instructions within milliseconds through spectral algorithms.
Multi-Dimensional Deep Screening
Traditional color sorting is just the first step. Nowadays, intelligent color sorter machines are more like all-round quality inspectors. Besides color, they can also screen based on the shape, size, and even the external texture of the materials.
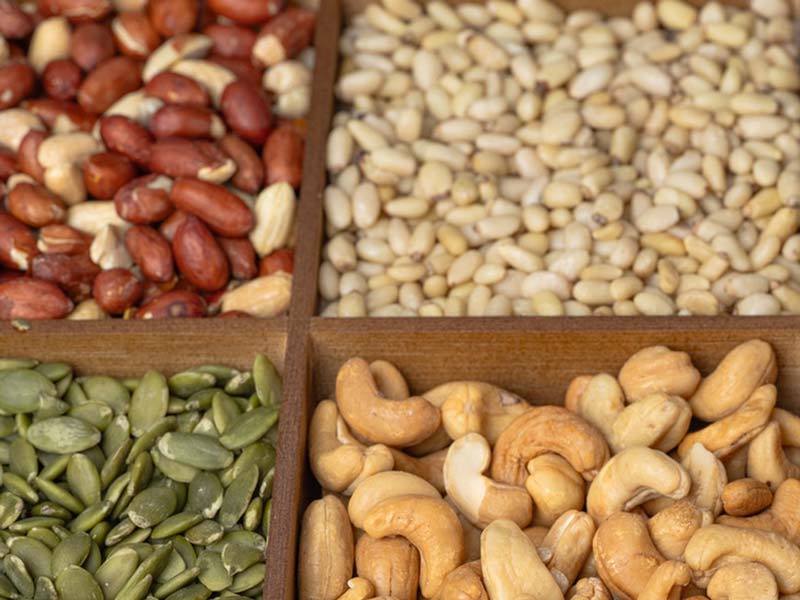
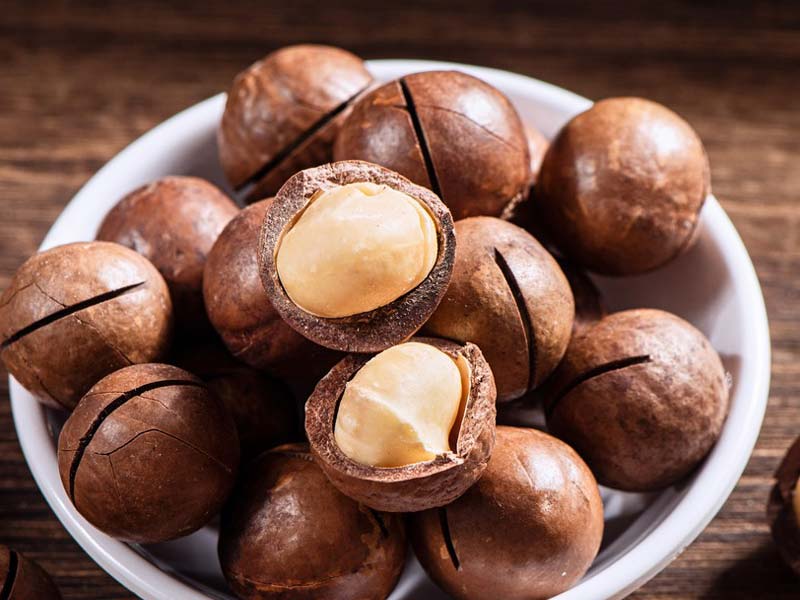
For example, in nut processing, it can precisely distinguish between intact nuts and broken nuts; in grain sorting, it can remove impurities with abnormal shapes. This over 99% screening rate has built a solid quality defense line for enterprises.
Dual Optimization of Efficiency and Cost
Many factory owners often struggle with the initial investment in equipment at the beginning. However, from the perspective of long-term operation logic, color sorting machines are actually the best “money-saving assistant”.
A Quantum Leap in Production Capacity
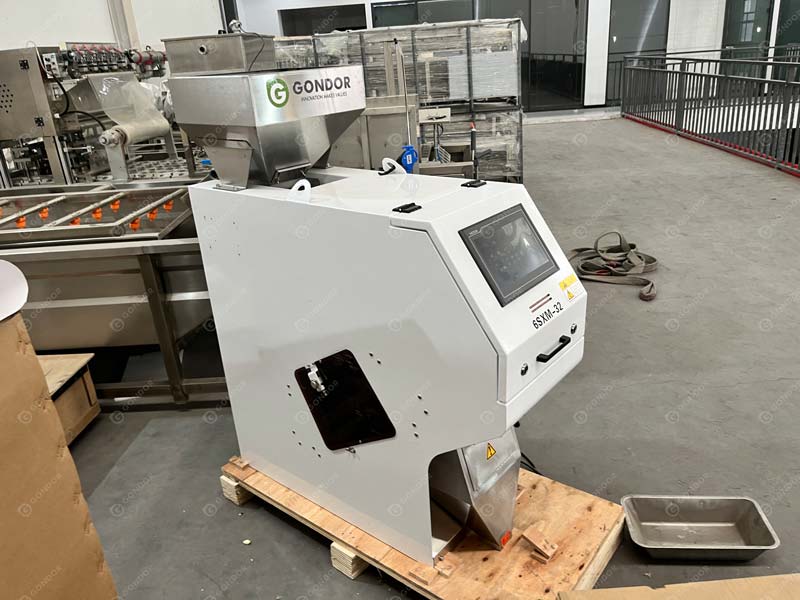
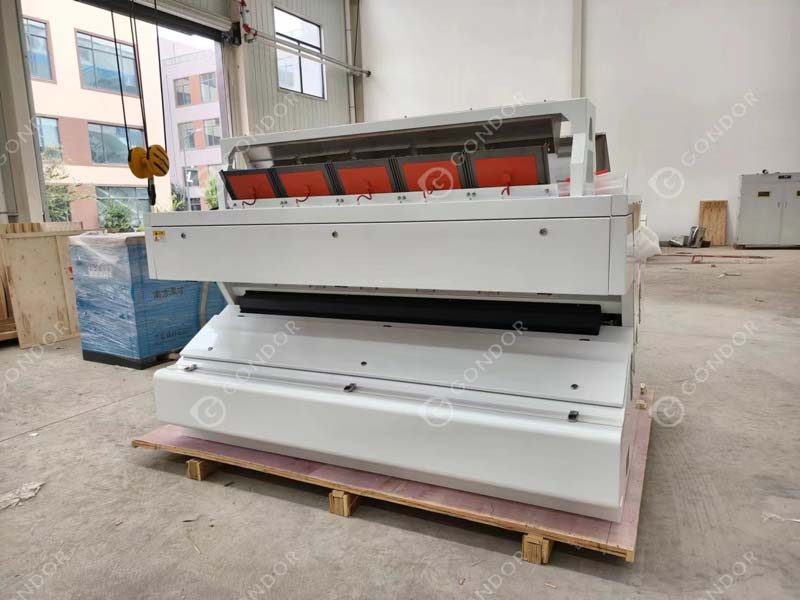
Even the most experienced sorter has a limited working time. However, Gondor’s color sorter machines, depending on the model, can easily increase their throughput from 0.5 tons per hour to 18 tons. This means that one machine can replace the labor output of dozens of workers, and it doesn’t need to rest, and can operate continuously 24/7.
The Ultimate Compression of Loss Rate
During manual sorting, the “misclassification” phenomenon often occurs—high-quality materials are mistakenly regarded as defective products and discarded. Our precise air jetting system can achieve targeted and precise strikes, only blowing away the defective materials.
This extremely low loss rate can offset the raw material costs accumulated over a period of long-term large-scale production within half a year, often enough to cover the purchase cost of the machines.
Application Scenarios of Color Sorter Machine
Color sorter machine can be easily applied to various industries.
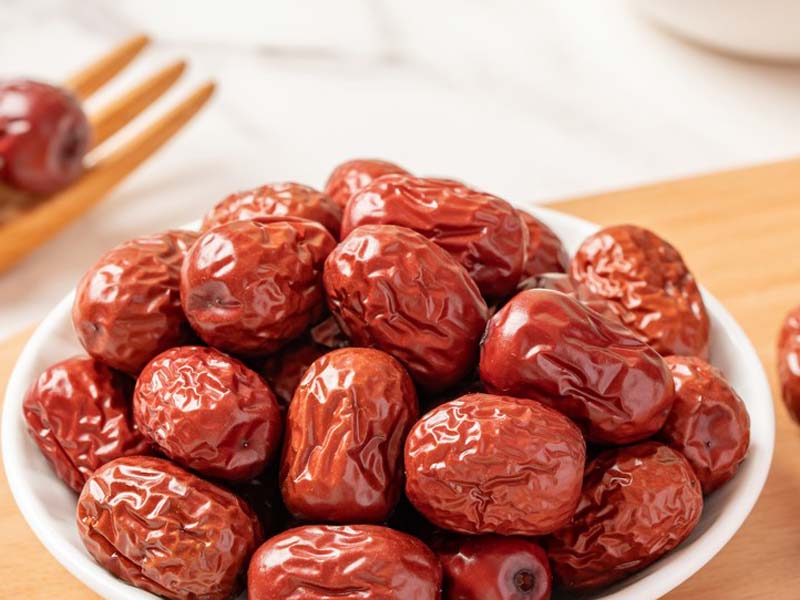
- Dehydrated Vegetables and Fruits: For dehydrated onions, carrot slices or dried fruits, color consistency is the key to grading pricing. The color sorter machine can remove the yellowed, dried or spotted parts, making the finished products look appealing.
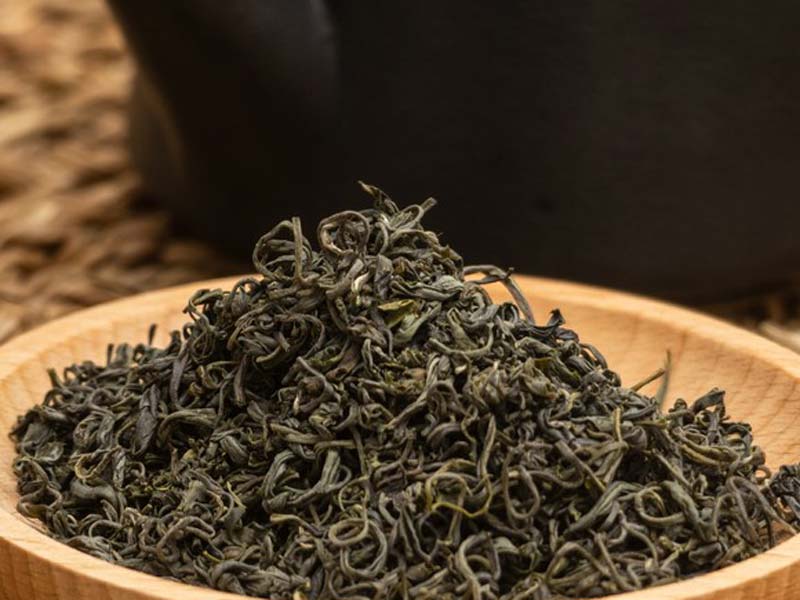
- Precision Crops: In the tea, seed, and nut industries, rice color sorter machine has significantly enhanced the value of products by detecting extremely subtle color differences.
Gondor: Your Intelligent Sorting Partner
In the era of automation, choosing the right partner is more important than selecting the machines themselves.
Gondor is committed to providing solutions that are not only “usable”, but also “easy to use”. Our color sorter incorporates an intelligent cloud detection system, which enables you to remotely monitor operating parameters such as air pressure and light sources, preventing malfunctions before they occur. This stability and durability are the core factors that enable us to establish a foothold in the highly competitive food machinery market.
If you are facing problems such as low sorting efficiency or quality fluctuations, why not have a chat with our experts? Gondor offers you customized sorting solution suggestions to help your factory achieve a true intelligent upgrade.